In the demanding environment of industrial workspaces, the importance of high-visibility apparel cannot be overstated. Specialized gear, such as reflective construction pants, serves as a critical line of defense for workers operating in low-light conditions or high-traffic zones. By enhancing a worker's visibility to vehicle operators and heavy machinery, these garments significantly reduce the risk of on-site accidents.
The evolution of safety wear has shifted from simple fluorescent fabrics to integrated systems that prioritize both visibility and environmental protection. Modern standards now demand a synergy between retro-reflective materials and durable textiles that can withstand the rigors of construction, mining, and roadwork. This intersection of safety and durability ensures that professionals remain protected regardless of the weather or the complexity of their tasks.
Understanding the technical specifications of reflective construction pants allows procurement managers and safety officers to make informed decisions that balance cost-efficiency with life-saving performance. From the choice of polyester blends to the application of PU coatings for water resistance, every detail contributes to the overall safety ecosystem of a modern industrial site.
Global Industry Context of Reflective Construction Pants
On a global scale, the demand for high-visibility clothing is driven by increasingly stringent occupational health and safety (OHS) regulations. According to international safety standards such as ISO 20471, the use of reflective construction pants is not merely a recommendation but a requirement in many jurisdictions to prevent fatalities in infrastructure projects. As urbanization accelerates across Asia and Africa, the volume of roadside construction has surged, making high-visibility gear a cornerstone of urban safety management.
The industrial challenge lies in the environmental diversity of construction sites. Workers often face a combination of extreme cold, heavy rain, and abrasive materials, which can degrade the reflective properties of their gear. Consequently, the industry is moving toward garments that offer multi-functional protection—combining the visibility of reflective tapes with the durability of PU-coated polyester and the warmth of detachable linings.
Defining the Standard for Reflective Construction Pants
Reflective construction pants are specialized lower-body garments designed to increase the wearer's visibility in hazardous environments. Unlike standard work trousers, these are engineered with retro-reflective materials that bounce light back to its source, such as vehicle headlights, ensuring that the worker is seen from hundreds of meters away. They typically combine fluorescent background colors—such as neon yellow or orange—with silver reflective strips.
In the context of modern industry, these garments are an essential component of Personal Protective Equipment (PPE). They address the critical need for "conspicuity," which is the ability of a person to be noticed against a complex background. This is particularly vital in nighttime operations or during inclement weather where visibility is severely reduced by fog, rain, or snow.
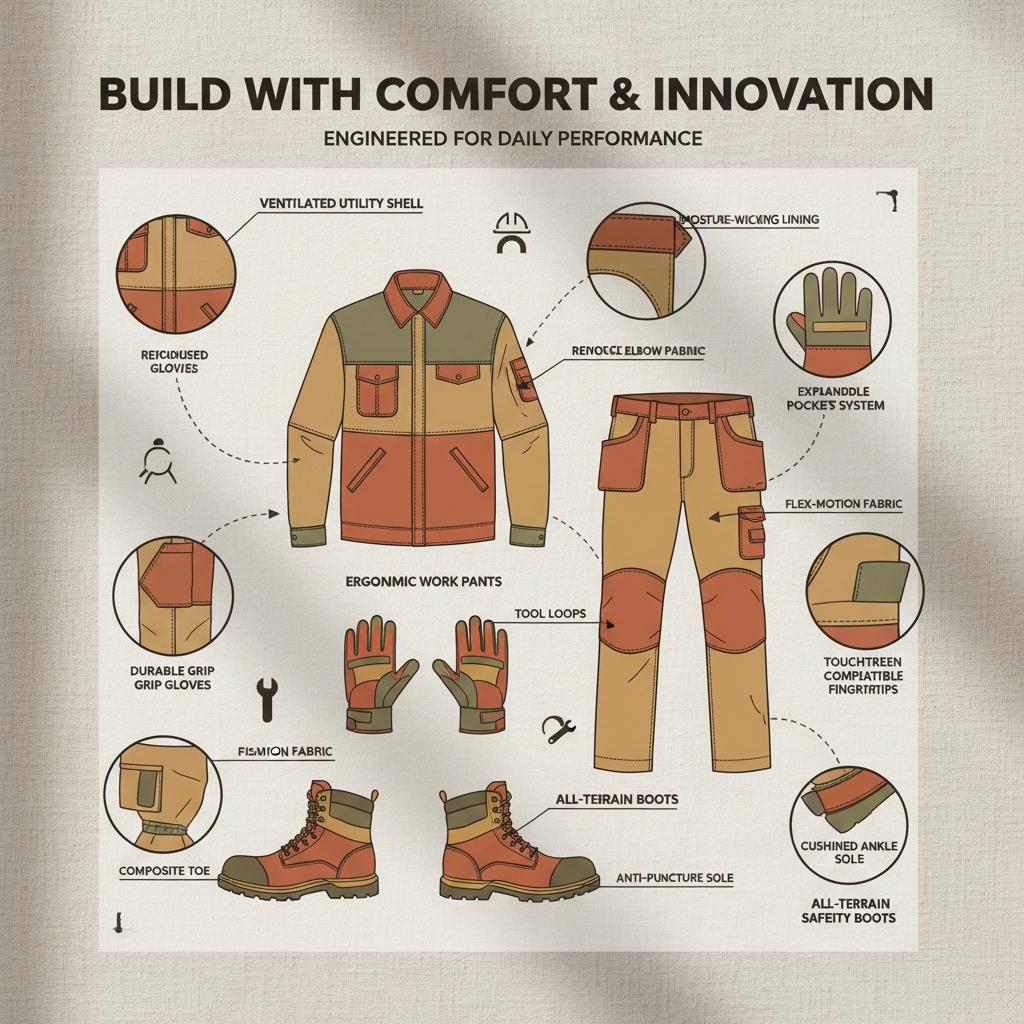
Beyond visibility, the modern definition of these pants includes ergonomic design and material resilience. For example, integrating 100% polyester with a PU coating provides a necessary waterproof barrier, while breathable mesh linings prevent overheating during intense physical exertion, ensuring that safety does not come at the expense of comfort.
Core Components of High-Visibility Safety Wear
The effectiveness of reflective construction pants depends heavily on material selection. The outer shell is typically constructed from high-density polyester, which provides the structural integrity needed for heavy-duty work. When treated with a PU coating, the fabric becomes a fortress against moisture and wind, ensuring the wearer stays dry in rain or sleet.
Another core component is the adaptability of the thermal system. For winter use, the integration of detachable linings—such as a 100% polyester padding jacket or a polar fleece layer—allows workers to customize their warmth. This modularity is crucial for those who transition between cold outdoor sites and warmer indoor environments throughout the day.
Finally, the reflective tape itself must meet strict luminance standards. These tapes are strategically placed around the ankles and thighs to outline the human form, which helps drivers distinguish a human from a stationary object. The synergy between the breathable mesh lining and the waterproof shell ensures that the reflective construction pants remain comfortable during extended shifts.
Practical Applications Across Industrial Sectors
The application of high-visibility gear extends far beyond simple roadwork. In large-scale mining operations, where heavy haul trucks operate in dusty or dark tunnels, the use of reflective gear is a mandatory safety protocol. Similarly, in airport ground handling and logistics hubs, where aircraft and forklifts move constantly, the visibility provided by these garments is the primary tool for preventing collisions.
In urban infrastructure projects, such as subway construction or bridge repair, workers often operate in "grey zones" where artificial lighting is inconsistent. The ability of these garments to reflect minimal light makes them indispensable for nighttime maintenance crews. Whether it is a mountain expedition for surveying or a city-center road repair, the versatility of waterproof and insulated safety wear ensures consistent protection.
Performance Metrics of High-Visibility Gear
Long-Term Value of Professional Safety Gear
Investing in high-quality reflective construction pants yields tangible long-term value by reducing workplace injuries and lowering insurance premiums for companies. When gear is constructed from OEKO-TEX 100 certified materials, it not only ensures safety but also guarantees that the textiles are free from harmful substances, improving the long-term skin health of the wearer.
From a psychological perspective, providing workers with professional, high-performing gear fosters a culture of safety and trust. When a worker feels protected against the elements—thanks to waterproof shells and insulated linings—their focus increases, leading to higher productivity and a reduction in human error caused by cold-induced fatigue or discomfort.
Future Innovations in Reflective Textile Technology
The future of safety apparel is moving toward "smart textiles." We are seeing the integration of LED strips and sensor-based lighting into reflective construction pants, which can blink or change color to alert supervisors of a worker's fall or distress. This digital transformation is turning passive safety gear into active communication tools.
Sustainability is another major trend. The industry is transitioning toward recycled polyester and biodegradable PU coatings to reduce the environmental footprint of PPE. By utilizing closed-loop manufacturing processes, brands can produce high-visibility gear that is both eco-friendly and compliant with the most rigorous safety standards.
Additionally, advancements in nanotechnology are creating "self-cleaning" fabrics. These materials repel oil, dirt, and grime—the very substances that typically dull the reflective properties of safety wear. This ensures that the visibility of the garment remains peak throughout its lifecycle, reducing the frequency of replacements.
Challenges and Solutions in Safety Apparel Maintenance
One of the primary challenges with reflective construction pants is the degradation of the reflective tape over time. Frequent washing and exposure to abrasive surfaces can cause the glass beads or prisms in the tape to wear down, significantly reducing visibility. To solve this, industry experts recommend specialized cleaning agents that do not strip the reflective coating.
Another common issue is the balance between waterproofing and breathability. Many cheap waterproof pants trap sweat, leading to "internal dampness" that can cause hypothermia in winter. The solution lies in using a high-performance polyester mesh lining that facilitates air flow while the outer PU layer keeps external water out.
Finally, the "one size fits all" approach often fails in safety gear, as ill-fitting pants can be a tripping hazard. Implementing a wider range of sizes (from 38 to 64) and utilizing adjustable waistbands ensures that the reflective elements remain in the correct anatomical position to be seen by others.
Analysis of Maintenance and Performance for Safety Apparel
| Maintenance Factor |
Common Challenge |
Recommended Solution |
Impact Score (1-10) |
| Reflective Tape |
Abrasive Wear |
Reinforced Stitching |
9 |
| Waterproofing |
PU Coating Peeling |
High-Temp Bonding |
8 |
| Thermal Control |
Overheating |
Detachable Linings |
10 |
| Fabric Breathability |
Moisture Build-up |
Polyester Mesh Lining |
7 |
| Fit & Ergonomics |
Limited Mobility |
Expanded Size Range |
8 |
| Color Retention |
UV Fading |
UV-Stabilized Dyes |
6 |
FAQS
Replacement depends on the wear level of the reflective tapes. If the tapes show significant cracking, peeling, or loss of luminance under a light test, they should be replaced immediately. On average, in heavy-duty construction environments, a full replacement every 6 to 12 months is recommended to maintain safety standards.
Yes, but with precautions. It is advised to wash them inside-out on a gentle cycle using mild detergents. Avoid bleach and high-temperature drying, as extreme heat can melt the PU coating and damage the retro-reflective beads, reducing the garment's effectiveness.
Detachable linings, such as polar fleece or padding, allow the worker to adapt to fluctuating temperatures. This prevents overheating during high-activity periods while ensuring warmth during static tasks in winter, making the gear suitable for multi-seasonal use.
PU coatings are designed for waterproofing and windproofing, which naturally restricts air flow. To counter this, professional gear incorporates a polyester mesh lining that moves moisture away from the skin, providing a balance between external protection and internal breathability.
Quality professional gear is designed to meet ISO 20471 or ANSI/ISEA 107 standards. Additionally, certifications like OEKO-TEX 100 ensure the materials are safe for human skin, which is essential for workers wearing these garments for 8-12 hours a day.
Both are effective, but the choice usually depends on the background. Yellow provides high contrast against urban concrete and greenery, while orange is often preferred for highway work as it contrasts better against the blue sky and grey asphalt.
Conclusion
In summary, reflective construction pants represent a critical synthesis of visibility, durability, and thermal protection. By utilizing advanced materials like PU-coated polyester and modular lining systems, these garments protect workers from both environmental hazards and accidental collisions. The long-term value of such gear lies in its ability to reduce risk, enhance worker comfort, and comply with global safety regulations.
Looking forward, the integration of smart textiles and sustainable manufacturing will further elevate the standard of PPE. For companies aiming to optimize their safety protocols, investing in certified, high-performance safety wear is the most effective way to safeguard their human capital. We invite you to explore our full range of industrial solutions. Visit our website: www.jidegarment.com